Phase Diagrams

phase diagrams worksheet, phase diagrams khan academy, phase diagrams and phase changes, phase diagrams for water, phase diagrams differential equations, phase diagrams critical point, phase diagrams and density, phase diagrams geology, phase diagrams practice, phase diagrams materials, phase diagrams, phase diagrams chemistry, phase diagrams ap chemistry, phase diagrams answer key, phase diagrams ap chem, phase diagrams answers, phase diagrams and physical states, phase diagrams and physical states chapter 10, phase diagrams alloys, phase diagrams asm, what is a phase diagrams, phase diagrams boiling point, phase diagrams book, phase diagrams binary, phase diagrams binary eutectic systems, phase diagrams binary system, phase diagrams binary alloys, phase diagrams basics, phase diagrams boron nitride, phase boundary diagrams, phase diagrams of binary titanium alloys, phase diagrams chemquest 9, phase diagrams chemquest 4 answers, phase diagrams calculations, phase diagrams chemistry pdf, phase diagrams co2, phase diagrams critical thinking questions, phase diagrams chemistry worksheet, phase diagrams composition, phase diagrams cooling curves, fe-c phase diagrams, phase diagrams density, phase diagrams database, phase diagrams definition, phase diagrams degrees of freedom, phase diagrams doitpoms, phase diagrams distillation, phase diagrams draw, phase diagrams for dummies, phase equilibria diagrams database, phase diagrams explanation, phase diagrams eutectic, phase diagrams examples, phase diagrams economics, phase diagrams eutectic systems, phase diagrams equilibrium, phase diagrams engineering, phase diagrams explained geology, phase diagrams exam questions, phase diagrams explained youtube, phase diagrams for ceramists, phase diagrams for binary alloys, phase diagrams for metals, phase diagrams for ceramists pdf, phase diagrams for binary alloys okamoto, phase diagrams from cooling curves, phase diagrams for water and carbon dioxide, phase diagrams for lead free solder alloys, phase diagrams geochemistry, phase diagrams for geoscientists, ternary phase diagrams geology, phase diagrams for geoscientists an atlas of the earth's interior, phase diagrams of gases, binary phase diagrams geology, chemguide phase diagrams, phase diagrams r geology, phase diagrams history, phase diagrams how to read, phase diagrams h2o, phase diagrams hydrogen, phase diagrams hydrates, phase diagrams hydrogen storage, phase diagrams heat, phase diagrams and heterogeneous equilibria a practical introduction, phase diagrams and heating curves, phase diagrams and heating curves worksheet, phase diagrams in chemistry, phase diagrams in metallurgy their development and application, phase diagrams in material science, phase diagrams in metallurgy, phase diagrams in metallurgy pdf, phase diagrams in metallurgy rhines, phase diagrams in economics, phase diagrams in metallurgy rhines pdf, phase diagrams igneous petrology, phase diagrams in advanced ceramics pdf, chemistry i phase diagrams water & co2, bull alloy phase diagrams journal, bulletin of alloy phase diagrams journal, j alloy phase diagrams, phase diagrams key, phase diagrams and kinetics leonid zhigilei, phase diagrams worksheet key, computer calculation of phase diagrams kaufman, computer calculation of phase diagrams kaufman pdf, known phase diagrams, phase diagrams lever rule, phase diagrams lecture notes, phase diagrams lecture, phase diagrams labeled, phase diagram lead tin, phase diagrams lines, phase diagrams lead, phase diagrams lattice, phase diagrams lipid, phase diagrams mineralogy, phase diagrams matlab, phase diagrams metallurgy, phase diagrams material science ppt, phase diagrams melting point, phase diagrams mono component and binary systems, phase diagrams metals, phase diagrams materials science and technology, phase diagrams made easy, phase diagrams notes, phase diagrams nptel, phase diagrams nptel pdf, phase diagram normal boiling point, phase diagrams nist, phase diagrams non ideal solutions, phase equilibria diagrams nist, phase diagrams of nanoalloys influence of size and morphology, phase diagrams of nanometer-sized particles in binary systems, poly(n-isopropylacrylamide) phase diagrams fifty years of research, phase diagrams of water, phase diagrams of water and carbon dioxide, phase diagrams of metals, phase diagrams of pure substances, phase diagrams of the elements, phase diagrams of one component systems, phase diagrams of alloys, phase diagrams of binary nickel alloys, phase diagrams of carbon dioxide, phase diagrams of binary hydrogen alloys, phase diagrams problems, phase diagrams pogil, phase diagrams petrology, phase diagrams practice problems, phase diagrams ppt, phase diagrams practice skill practice 4, phase diagrams ppt presentation, phase diagrams physical chemistry, phase diagrams pdf, phase diagrams quiz, phase diagrams questions, phase diagrams of quasi binary systems of the type, phase diagrams of quaternary iron alloys, phase diagrams of quasi binary systems, phase diagrams multiple choice questions, quaternary phase diagrams, quasi binary phase diagrams, phase diagrams rhines, phase diagrams review, phase diagrams reactions, phase diagrams resonance, phase diagrams reddit, phase rule diagrams, phase diagrams igneous rocks, phase diagrams steel, phase diagrams software, phase diagrams summary, phase diagrams sgte, phase diagrams southampton, phase diagrams solved problems, phase diagrams solid solutions, phase diagrams solid state chemistry, phase diagrams slideshare, phase diagrams solution, phase diagrams thermodynamics, phase diagrams teaching transparency worksheet 41, phase diagrams tutorial, phase diagram triple point, phase diagram tie line, phase diagram triangle, phase diagram test, phase diagram terms, phase diagram t butyl alcohol, phase diagram tert butyl alcohol, phase diagrams understanding the basics, phase diagrams understanding the basics pdf, phase diagrams understanding the basics by f. c. campbell, phase diagrams understanding the basics download, phase diagrams uses, phase diagrams understanding the basics ebook, phase diagrams cambridge university, why are phase diagrams useful, analysis phase uml diagrams, interactive 3d phase diagrams using jmol, phase diagrams video, phase diagrams video lectures, phase diagrams vapor pressure, phase change diagrams video, interpreting phase diagrams video, phase diagrams constant volume, 3 phase vector diagrams, phase diagrams of binary vanadium alloys, phase diagrams for ceramists volume 1, binary alloy phase diagrams vol. 1, phase diagrams water, phase diagrams wikipedia, phase diagram weight percent, phase diagrams water and co2, phase diagrams water carbon dioxide, phase diagrams website, phase diagrams weight, phase diagrams water mixtures, phase diagram temperature composition, phase diagrams youtube, young phase diagrams of the elements, phase diagrams for zirconium and zirconia systems, phase diagrams 12.1 worksheet, phase diagrams 12.1 worksheet answers, phase diagrams 12.4, phase diagrams section 12.4, phase diagrams chapter 12, phase diagrams chapter 10, phase diagrams part 1, phase diagrams chapter 12 answers, phase diagrams for ceramists 1964, phase diagrams for ceramists 1969 supplement, chemistry 1 phase diagrams water and co2, 1 phase wiring diagrams, binary alloy phase diagrams 2nd edition, phase change diagrams objective 2.11, 2 phase diagrams, 2d phase diagrams, 2 component phase diagrams, 2 component system phase diagrams, spin-2 phase diagrams, phase diagrams 3d, phase diagrams 3 component systems, 3 phase diagrams, 3.091 phase diagrams, 3 phase wiring diagrams, 3 phase wiring diagrams motors, 3 phase schematic diagrams, 3 phase phasor diagrams, 3 phase transformer diagrams, 3 phase motor diagrams, 3 phase power diagrams, 3 component phase diagrams, 3 phase electrical diagrams, 4 phase diagrams, chemquest 4 phase diagrams answer key, chemquest 4 phase diagrams, skill practice 4 phase diagrams answers, skill practice 4 phase diagrams answer key, worksheet #4 phase change diagrams, 7 types of binary phase diagrams, chapter 8 phase diagrams, chapter 9 phase diagrams problem solutions, chapter 9 phase diagrams, chemquest 9 phase diagrams, chapter 9 phase diagrams ppt, chapter 9 phase diagrams pdf, chapter 9 phase diagrams solutions, chemquest 9 phase diagrams answers, skill practice 9 phase diagramsa

Phase Diagram

  • It is also known as equilibrium diagram.

  • The plots showing relations between phases in equilibrium versus composition, pressure and temperature are called phase diagrams.

  • The composition is plotted on X-axis and temperature is plotted on Y-axis at any specified pressure. Pressure is generally taken atmospheric.

    • Water in liquid or vapor state is single phase.

    • Ice floating on water is an example two phase system.


Gibbs Phase rule

The number of degrees of freedom, F (no. of independently variable factors),number of components, C, and number of phases in equilibrium, P, are related by :

  • Gibbs phase rule :


F = C – P + 2

  • Number of external factors = 2 (pressure and temperature).


For metallurgical system, pressure has no appreciable effect on phase equilibrium and hence,

F = C – P + 1

One component system 

  • The simplest phase diagram is the water which is a one component system.

  • It is also known as pressure-temperature or P-T diagram.

  • Two phases exist along each of the three phase boundaries.

  • At low pressure (0.006 atm) and temperature (0.01 °C) all the three phases coexist at a point called triple point.


Water phase diagram is shown in the following figure.

03-Phase-diagrams (1)

Binary Phase diagrams

  • A binary phase is a two component system.

  • Binary phase diagrams are most commonly used in alloy designing.

  • The simplest binary system is the Cu-Ni which exhibits complete solubility in liquid and solid state.


The Cu-Ni equilibrium phase diagram is shown below.

03-Phase-diagrams (2)

  • The line above which the alloy is liquid is called the liquidus line. At temperature just below this line crystals of α solid solution start forming.

  • The line below which solidification completes is called solidus line. Hence, only α solid solution exists at any temperature below the solidus line.

  • The intermediate region between liquidus and solidus lines is the two-phase region where liquid and solid coexist.


It can be noted that the two metals are soluble in each other in the entire range of compositions in both liquid and solid state. This kind of system is known as‘Isomorphous’ system.

There are 5 invariant reactions occurring in binary phase system:

  • Eutectic reaction,

  • Eutectoid reaction,

  • Peritectic reaction,

  • Peritectoid reaction, and

  • Monotectic reaction.


Eutectic Point

When a liquid phase changes into two different solid phases during cooling or two solid phases change into a single liquid phase during heating, this point is known as eutectic point and this temperature is known as eutectic temperature.

In the eutectic system between two metals A and B, two solid solutions, one rich in A (α) and another rich in B (β) form. In addition to liquidus and solidus lines there are two more lines on A and B rich ends which define the solubility limits B in A and A in B respectively. These are called solvus lines.

Three phases (L+ α+ β) coexist at point E. This point is called eutectic point or composition. Left of E is called hypoeutectic whereas right of E is called hypereutectic.

Equation for Eutectic:

03-Phase-diagrams (1)

Phase Diagram characteristic of Eutectic:

03-Phase-diagrams (4)

Eutectoid Point

When a solid phase changes into two solid phases during cooling and vice-versa that point is known as eutectoid point and temperature at this reaction occurs known as Eutectoid temperature.

03-Phase-diagrams (3)

Three phases (L+ α+ β) coexist at point E. This point is called eutectic point or composition. Left of E is called hypoeutectic whereas right of E is called hypereutectic.

Equation for Eutectoid:

03-Phase-diagrams (2)

Phase Diagram characteristic of Eutectoid:

03-Phase-diagrams (5)

Peritectic Point

A binary system when solid and liquid phases changes solid phase on cooling and vice-versa on heating, then state of system is known as peritectic point.

Equation for Peritectic:

03-Phase-diagrams (3)

Phase Diagram characteristic of Periterctic:

03-Phase-diagrams (6)

Peritectoid Point

If a binary phase diagram when two solid phases changes to one solid phase, then state of system is known as peritectoid point.

Equation for Peritectiod:

03-Phase-diagrams (4)

Phase Diagram characteristic of Pertitectoid:

03-Phase-diagrams (7)

Monotectic Point

Another three phase invariant reaction that occurs in some binary system is monotectic reaction in which a liquid transforms to another liquid and a solid. L1→ L2 + α

Equation for Montectic:

03-Phase-diagrams (5)

Phase Diagram characteristic of Monotectic:

03-Phase-diagrams (8)


All Material Science Books PDF :

[catlist name="material science"]

Heat Treatment


Heat treatment of a metal or alloy is a technological procedure, including controlled heating and cooling operations, conducted for the purpose of changing the alloy micro-structure and resulting in achieving required properties.


Normalising


  • For this process, the metal is placed in the furnace and heated to just above its 'Upper Critical Temperature'.

  • When the new grain structure is formed it is then removed from the furnace and allowed to cool in air as it cools new grains will be formed.

  • These grains, although similar to the original ones, will in fact be smaller and more evenly spaced.

  • Normalising is used to relieve stresses and to restore the grain structure to normal.


This is particularly useful after heavy machining where grains may have become stressed or after the prolonged heating of a forging process has allowed the grains to grow large.


Quenching


  • It is a heat treatment when metal at a high temperature is rapidly cooled by immersion in water or oil.

  • Quenching makes steel harder and more brittle, with small grains structure.


Annealing (Softening)


  • Annealing is a heat treatment procedure involving heating the alloy andholding it at a certain temperature (annealing temperature), followed bycontrolled cooling.

  • Annealing results in relief of internal stresses, softening, chemical homogenising and transformation of the grain structure into more stable state.

  • The annealing process is carried out in the same way as normalising, except that the component is cooled very slowly. This is usually done by leaving the component to cool down in the furnace for up to 48 hours.

  • Annealing leaves the metal in its softest possible state and is usually carried out to increase ductility prior to cold working or machining.

  • Annealing is carried out in different stages which are classified as:

    • Stress relief (recovery) 

      • A relatively low temperature process of reducing internal mechanical stresses, caused by cold-work, casting or welding.

      • During this process atoms move to more stable positions in the crystal lattice. Vacancies and interstitial defects are eliminated and some dislocations are annihilated.

      • Recovery heat treatment is used mainly for preventing stress-corrosion cracking and decreasing distortions, caused by internal stresses.


    • Recrystallization 

      • It can be easily said to be alteration of the grain structure of the metal.

      • If the alloy reaches a particular temperature (recrystallization or annealing temperature) new grains start to grow from the nuclei formed in the cold worked metal. The new grains absorb imperfections and distortions caused by cold deformation. The grains are equi-axed and independent to the old grain structure.

      • As a result of recrystallization mechanical properties (strength, ductility) of the alloy return to the pre-cold-work level.

      • The annealing temperature and new grains size are dependent on the degree of cold-work which has been conducted. The more is the cold-work degree, the lower is the annealing temperature and the fine recrystallisation grain structure.

      • Low degrees of cold-work (less than 5%) may cause formation of large grains. Usually the annealing temperature of metals is between one-third to one-half of the freezing point measured in Kelvin (absolute) temperature scale.


    • Grain growth (over-annealing, secondary recrystallization)

      • Growth of the new grains at the expense of their neighbours, occurring at temperature, above the recrystallization temperature.


This process results in coarsening grain structure and is undesirable.


04-Heat-treatment (1)


Hardening


  • Hardening also requires the steel to be heated to its upper critical temperature (plus 50°C) and then quenched.

  • The quenching is to hold the grains in their solid solution state calledAustenite; cooling at such a rate (called the critical cooling rate) is to prevent the grains forming into ferrite and pearlite.

  • Hardening is a process of increasing the metal hardness, strength,toughness, fatigue resistance.

  • The rate of cooling affects the hardness of the metal, in that the faster the cooling rate, the greater the hardness.

  • The cooling liquid can therefore be selected to suit the hardness required. If a steel is quenched too rapidly it may crack, this is especially true with thin walled components.

    • Strain hardening (work hardening)

      • Strengthening by cold-work (cold plastic deformation),

      • It causes increase of concentration of dislocations, which mutually entangle one another, making further dislocation motion difficult and therefore resisting the deformation or increasing the metal strength.


    • Grain size strengthening (hardening)

      • Strengthening by grain refining.

      • Grain boundaries serve as barriers to dislocations, raising the stress required to cause plastic deformation.


    • Solid solution hardening

      • Strengthening by dissolving an alloying element.

      • Atoms of solute element distort the crystal lattice, resisting the dislocations motion. Interstitial elements are more effective in solid solution hardening, than substitution elements.


    • Dispersion strengthening 

      • Strengthening by addition of second phase into metal matrix.

      • The second phase boundaries resist the dislocations motions, increasing the material strength.

      • The strengthening effect may be significant if fine hard particles are added to a soft ductile matrix (composite materials).


    • Hardening as a result of Spinodal decomposition

      • Spinodal structure is characterized by strains on the coherent boundaries between the spinodal phases causing hardening of the alloy.


    • Precipitation hardening (age hardening)

      • Strengthening by precipitation of fine particles of a second phase from a supersaturated solid solution.

      • The second phase boundaries resist the dislocations motions, increasing the material strength. The age hardening mechanism in Al-Cu alloys may be illustrated by the phase diagram of Al-Cu system.

      • When an alloy Al-3%Cu is heated up to the temperature TM, all CuAl2 particles are dissolved and the alloy exists in form of single phase solid solution (α-phase). This operation is called solution treatment.

      • Slow cooling of the alloy will cause formation of relatively coarse particles of CuAl2 intermetallic phase, starting from the temperature TN.

      • However if the the cooling rate is high (quenching), solid solution will retain even at room temperature TF. Solid solution in this non-equilibrium state is called supersaturated solid.

      • Obtaining of supersaturated solid solution is possible when cooling is considerably faster, than diffusion processes. As the diffusion coefficient is strongly dependent on the temperature, the precipitation of CuAl2from supersaturated solution is much faster at elevated temperatures (lower than TN).This process is called artificial aging. It takes usually a time from several hours to one day. When the aging is conducted at the room temperature, it is called natural aging.


04-Heat-treatment (2)

Tempering


  • As there are very few applications for very hard and brittle steel, the hardness and brittleness needs to be reduced. The process for reducing hardness and brittleness is called tempering.

  • Tempering consists of reheating the previously hardened steel.

  • During this heating, small flakes of carbon begin to appear in the needle like structure. (See below) This has the effect of reducing the hardness and brittleness.

  • The temperature to which the steel is reheated depends on the hardness required by the application of the component. The higher the tempering temperature, the less hard will be the resulting steel.


04-Heat-treatment (3)

If the steel is polished before tempering, the range of oxide colours that the steel goes through during heating can be used as a guide to its temperature.


Stress Relieving


  • When a metal is heated, expansion oc­curs which is more or less proportional to the temperature rise. Upon cooling a metal, the reverse reaction takes place. That is, a contraction is observed.

  • When a steel bar or plate is heated at one point more than at another, as in welding or during forging, internal stresses are set up.

  • During heating, expansion of the heated area cannot take place unhindered, and it tends to deform. On cooling, contraction is prevented from taking place by the unyield­ing cold metal surrounding the heated area.

  • The forces attempting to contract the metal are not relieved, and when the metal is cold again, the forces remain as internal stresses. Stresses also result from volume changes which accompany metal transformations and precipitation.

  • The term stress has wide usage in the metallurgical field. It is defıned simply as bad or force divided by the cross-sectional area of the part to which the bad or force is applied.

  • Internal, or residual stresses, are bad because they may cause warping of steel parts when they are machined.


To relieve these stresses, steel is heated to around 1100 0F (595 0C) assuring that the entire part is heated uniformly, then cooled slowly back to room temperature. This procedure is called stress relief annealing, or merely stress relieving


Allotropic Forms of Steel


  • The temperature 723oC is known as Curie temperature, below it steel shows magnetic properties and above it steel becomes non-magnetic.

  • In the diagram, the carbon percentage is plotted on X-axis and temperature plotted on Y-axis.

  • The melting point of iron is about 1539oC. The melting temperature of iron varies with increasing carbon percentage.

  • The iron has carbon upto 2% known as steel. The cast-iron is a form of having 2 to 4.5% carbon. The iron has carbon upto 6.67% known as pig iron.


04-Heat-treatment (4)

Eutectcid Point


Eutectoid reaction in this diagram occurs when temperature 1oC and carbon is 0.83%. At this point a solid form iron (γ) changes into two solid forms α–iron and cementite (Fe3C).


04-Heat-treatment (5)


  • A eutectoid mixture of ferrite (α–iron) and cementite is known as pearlite. This is a microconstituent.

  • The fraction of ferrite in eutectoid steel is 88%.


Eutectic Point


  • In this diagram, the location of this point is at 1175oC temperature and 4.3% at the carbon. At this point eutectic reaction occurs.

  • In this reaction, a liquid phase changes two solid phases γ-iron (austenite) and cementite (FeC).

  • Peritectic reaction occurs at 1495oC and at this point carbon composition is 0.18%. This temperature is known as peritectic temperature.


All Heat Transfer Books PDF :

[catlist name="heat transfer"]


All Material Science Books PDF :

[catlist name="material science"]

Design a Projectile Launcher

Design a Projectile Launcher


Design a spring-loaded gun to shoot a projectile to your worst enemy. The conceptual design of this gun is shown on the next page.
• It consists of a commercially available pipe (1), 
• bottom cap (2) 
• with an opening for the trigger pin, trigger pin (3), 
• piston (4),
• threaded rod (5) 
• with a machined groove (6) to engage the trigger pin, 
• nut (7), 
• projectile (8), 
• helical spring (9) 
• and  aerodynamic projectile nose (10) of negligible weight.


 The projectile has a mass of 0.5 lbm. The target is located on the ground and 250 ft away. The gun will shoot from the ground level at an angle that maximizes the horizontal reach of the projectile. The spring must be preloaded (i.e. compressed) in order to install inside the gun and provide an initial compressive force. The force required to pull the trigger pin should be less than 50 lbf. 

The spring is compressed to solid length by tightening the nut with a power wrench. The trigger pin is inserted through the bottom cap and into the groove to secure the gun in the loaded position. The nut is then backed up all the way and the trigger pin pulled by hand to shoot.

Specify all design parameters listed below. Make all necessary choices and assumptions, which should be listed along with your calculations. Use sound engineering judgement. Provide a professionally written calculation package and schematics to get full credit. Use Excel, MathCAD or MathLab to facilitate design iterations and provide detailed screenshots of inputs and outputs. Comply with all notes listed on the cover page.

1) Projectile velocity and angle when exiting the gun.
2) Stroke or distance traveled by the piston to shoot.
3) Distance that the spring should be preloaded or compressed when installed.
4) Outside diameter (OD) and length of the projectile knowing that it’s made of aluminum 7075-T6 tubing having 1/8” wall thickness.
5) Diametral clearances between pipe and spring, and between pipe and projectile.
6) Internal diameter (ID) of the pipe. 
7) Mean diameter, wire diameter, material choice, spring constant, spring index, number of active coils, total number of coils, solid length, free length, pitch, maximum spring force, minimum spring force, maximum stress, static safety factor, critical length, weight, natural frequency and fatigue safety factor of the spring based on Gerber. 
8) If necessary, consider the use of nested springs, in which case, all the parameters listed in item 7) should be specified for each spring.
9) Nominal diameter, thread type and material choice for the threaded rod.
10) Rod groove dimensions.
11) Safety factor against tensile yielding of the rod thread and rod body.
12) Use your knowledge of dynamics to estimate the force generated on the nut upon impact and to relate projectile velocity to spring constant.
13) Safety factor against shearing the rod and nut threads.
14) Torque required to turn the nut in order to load the gun.
15) Force to pull the trigger pin.
16) Safety factor against shearing the trigger pin.
17) Gerber fatigue safety factor for the rod.


Solution


Projectile

To specify the dimensions of projectile, dimensions of pipe should be known. Schedule STD was randomly selected from the available standards schedules and pipe with various diameter range from 0.5 in to 5 in (nominal diameter) where examine and result are shown below


From the equation that density is equal to mass per unit volume, length and diameter of projectile can be selected.

L×t×(Douter-t)= ρ×π/m

Here diameter of the projectile should be kept 0.02 in less than the inner diameter of pipe for diametrical clearance and by this length can find out.


Outer diameter and length of the projectile is taken as 3.096 in and 1.72 in reason will be explain in lateral discussion. Internal diameter of the pipe is 3.5 in. 

To have the maximum range at a given velocity angle of projection should be 45 degree. So to have 250ft as maximum range angle should be 45 degrees and by using following formula, velocity of the projectile can be find out.

R=  (v^2×sin⁡〖2∝〗)/g
v = 89.68 ft/sec
Following equation show the relation between projectile velocity and spring constant
v= √((k ×x^2)/m)
Form this equation we can develop a relation
k ×x^2  = v^2  ×m = 4021.75

Spring design
While designing spring following formulas, consideration and assumptions were taken

Diametrical clearance = 0.02 in
Spring constant = 7
D mean = C ×d
D inner = D mean – d
K = G×d^4/(8D^3 N)
Total number of coils Nt = active coils Nv + 2
Free length = 2×solid length
Solid length = wire diameter  ×  Nt
Pitch = (free length-2d)/Nv
Force F max  = K ( free length – solid length)
Shear stresses in spring τ=8WDF/(πd^3 )
Factor of safety = Allowable stresses/ design stresses

Using above formulas calculations we carried out using different outer diameter with respect to pipe diameter, different wire diameter, different number of totals coils and different number of active coils.


From those entire calculations one with red mark is selected because this one set best with our pipe, required length of springs, number of coils and it provide sufficient force to projectile required velocity.
Output
• Outer diameter of spring = 3.5 in
• Inner diameter of spring = 2.211 in
• Sprig index = C = 7
• Wire diameter = d = 0.443 in
• Mean diameter = Dm = 2.65 in
• Nt = 6
• Nv = 4
• Shear modulus = G = 11500000 psi
• K = 735.863 lbm/in
• Compression distance = x = 2.34 in
• Solid length = 2.65 in
• Free length = 5.30 in 
• Pitch = 1.10 in
• Force = 1952.77 lbf
• Shear stresses = 185083 psi
• Mass = 2.18 lbm
• Frequency = 9.18 Hz
• FOS = 175000000/185083 = 5.40
Distance travel by the piston is equal to the compression distance of the spring equal to 2.34 in. preloading is done to make the nut and bolt tight and for this compression of 0.1 in will be enough.


Threaded Road
Threaded rod should be the one that can fit inside the spring and provide the sufficient power to compress the spring. From standard tables following Acme square threads were selected and analyzed for stresses and torque. Material of the rod is steel.

For Rod
Force on the rod is F = 1952 (spring force)
Steel yield point = 31200 psi
Area of rod = (π×d^2)/4 = 3.14 in^2
Stresses = force/area = 621 psi
FOS = yield stresses/stresses = 50.24 

For thread
Force on the rod is F = 1952 (spring force)
Steel yield point = 31200 psi
Area of threads from table = 1.824 in^2
Stresses = force/area = 1070.17 psi
FOS = yield stresses/stresses = 29.15
Torque requirement
As d = 2 in
Dm = 2 – pitch/2 = 1.875 in
Friction coefficient = 0.15 steel dry
Torque required to compresses the spring
T_r=  (F×dm)/2  ×(l+πfdm)/(πdm-fl)
T_r=434 lbfin
Maximum nominal shear stress in threads
τ =3F/(π d_r Nt ×pitch)
d_r=1.75 in
τ=2131.39 psi
Dividing this shear stress with torsional yield stresses 7800 psi we have FOS = 3.65

Rod groove dimension
Steel shear strength = 15600 psi
After the factor of safety = 2
Shear strength = 7800 psi
Shear Stress = force/area

So

Area = force / shear stress = 0.25 in^2
Area of square = ab = 2a = 0.25 in ^2
a = 0.125 in
Depth of groove should also be 0.125 in to compensate stresses. 


Trigger Pin 

Let pin is made of steel and its opening cavity is also made of steel. Friction between steel and steel is 0.42. Forces required to remove the pin is F =μ N where N is force applied by the spring so F = 819.84 lbf. As trigger pin made of the same dimension as groove on rod so the safety of factor for it will be same that is 2. 


Nut
As nut is also made of steel and has same thread dimensions as screw has so the torque and FOS for him is as follow.
τ =3F/(π d_r Nt ×pitch)
d_r=2 in
τ=1864 psi
Dividing this shear stress with torsional yield stresses 7800 psi we have FOS = 4.18
Upon impact of nut with wall of launcher force which act of nut is same force which spring has in it when it was in compresses form. Upon releasing same force will act on the nut when it hit the wall. 

ADDITIVE LAYER MANUFACTURING OF ENGINE CYLINDER BLOCK


Project 1- ADDITIVE LAYER MANUFACTURING OF ENGINE CYLINDER BLOCK


https://upload.wikimedia.org/wikipedia/commons/thumb/1/1f/CarterBMW1.JPG/220px-CarterBMW1.JPG
source: Wikipedia

Additive layer technology more commonly known as the 3D printing or layer by layer manufacturing technology is the most discussed and used (at small level) manufacturing method now a days. As engineers are trying to manufacture more and more products through additive layer manufacturing so in this post we will try to select a an additive layer manufacturing process for engine cylinder block by working on following steps

1. Study the current Manufacturing Process
2. Select one additive layer manufacturing process 
3. Study the new manufacturing process
4. Compare the present and new manufacturing processes
5. Conclude the result about the additive layer manufacturing of engine cylinder block


1.0 Introduction
Additive layer manufacturing process work opposite to the conventional subtractive method was parts are manufacture by removing the material from a work piece. In additive layer manufacturing the parts are made by combining the successive layer of material one over the other under a control environment [1]. Initially this method was mostly used for rapid prototyping but with time the manufacturer realized its importance and own they are used for the production of functional products [2]. Currently the additive layer manufacturing is basically used for the production of the equipment used in aerospace and high performance cars because of very high cost of the equipment used in this process [3]. 

Here a brief study about the suggestion of an additive layer manufacturing for the manufacturing of cylinder block of a V-6 engine has been conducted here. Before suggestion of the ALM process, the current manufacturing process and material requirements will be discuss along with the brief discussion of the product.

1.1 Cylinder Block
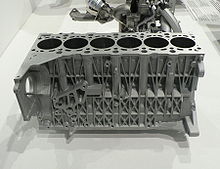
An engine block is the core of the engine which houses nearly all of the components required for the engine to function properly. The block is typically arranged in a “V,” inline, or horizontally-opposed (also referred to as flat) configuration and the number of cylinders range from either 3 to as much as 16. Because engine blocks are a critical component of an engine, it must satisfy a number of functional requirements. These requirements include lasting the life of the vehicle, housing internal moving parts and fluids, ease of service and maintenance, and withstand pressures created by the combustion process [4].


source: Wikipedia 


Figure 1 Cylinder Block of IC Engine

1.2 Material for Cylinder Block
Following are some of the properties that a material should have in order to process it for manufacturing of cylinder block [5]
• Cheap
• Good Cast ability 
• Good impressions
• Good Machine ability
• Rigid and strong
• Good abrasion resistance,
• Good corrosion resistance,
• High thermal expansion,
• High thermal conductivity,
• Low density.

Some of the material that are already in use in different manufacturing organization for production of cylinder block are cast iron, aluminum alloy and magnesium alloy. Aluminum alloys are now mostly used for high performance in light vehicle due to its low density and high strength [4] [8].

1.3 Manufacturing Process for Cylinder Block
There are number of manufacturing processes been used by different companies like Honda is using pressure die casting [6] and BMW is using sand casting [7] for their cylinder block production. Many other processes like machining from solid and lost form process are also being processed in different companies. Selection of the process really depends on the material and functional requirements of the engine cylinder block.

2.0 Current Manufacturing Process of Cylinder Block
The manufacturing process that will be discussed here is the sand casting and data mention below is being taken from the discovery channel documentary that show the complete manufacturing process of V-6 cylinder block [8]. 

Manufacturing process starts with the preparation of the sand and glue mixture that will be used for the production of cores. A single mold for a cylinder block is made up of 18 different cores and all are made for the master pattern made of steel. There is one main core with which all other 17 cores are attached. Iron liners are placed in the bores of the cylinder bore core, this help avoid abrasion. Some of the cores have to be glue to improve the strength and prevent the braking while assembling. Process of making and assembling and the cores are completely automated which decrease the time but increase the cost of operation.

After mold is complete the aluminum alloy ingots are melted in the gas fired furnace where temperature ranges up to 800 degree centigrade. Mold bores are heated with the electric current because the melted aluminum alloy bounds better with the hot metal. Molten aluminum alloys are feed from the bottom of the mold to avoid the oxide formation and can be a problem when molten material is feed from the top of the mold. 

After the solidification the mold is place in the oven can thermal sand reclaim oven where it spend six hours to dissolve al the glue and recover all the sand. Sand remains inside the cylinder block is removed by tilting the block sidewise. Extra material in the shape of riser will be removed by the help of CNC machines. CNC machines will be used to do the finishing process of the cylinder block.

Process up till now is a general process for the production of the every engine cylinder block. Further detailing and finishing will be done according to the use of the cylinder block. After completing the process a visual test is conducted to check for any defect present in the product.

3.0 Current Manufacturing Process Steps
Following are the steps arranged in the sequence for the manufacturing of engine cylinder block as explained in the above [8]
1. CAD Drawing
2. Mater Pattern Preparation
3. Preparing Sand and Glue Mixture
4. Core Production
5. Cores Assembly
6. Melting Aluminum
7. Pouring
8. Sand Recovery Oven
9. Primary Machining
10. Final Machining

3.1 CAD Drawings
First step is to create the detail CAD drawing of the engine cylinder block and then divide it into different section according to the manufacturing process to manufacture the master pattern of each section. This step required highly skilled labor and good CAD software which not cost much. Time of this process is usually in days and cost of the process is low to moderate

3.2 Master Pattern
Master pattern is required for each sand core used to make a complete sand mold for the casting a one complete engine cylinder block. There are 18 total master patterns, one for each core. Creating a master pattern required a third party because manufacturing master pattern required highly skilled labor and expansive machinery. Manufacturing time is usually in days for a single master pattern, so manufacturing 18 master patterns required at least 4-5 month. Cost of this process is very high but it is one time process [9].

3.3 Preparing Sand and Glue Mixture
A separate mixing machine is used for the preparing the sand and glue mixture. Quality of the mixture is really important as this thing define the surface finish and some defects in the final product [10]. Sand and glue are mixed in predetermined quantity due to which this step required low labor skills and have low operation cost but is a continuous process because new mold is required every time. 

3.4 Cores Production
To make a core, sand and glue mixture is blows into the cavity having master pattern. Here the sand and glue get hard with the help of gas which activities the hardener due to which sand takes the shape of the master pattern. This process is fully automatic which increase the rate of production but this come at increase cost in term of robots installation and operation [8]. This process of core making is continuous process because core need to broke in order to remove the cylinder block [10].

3.5 Core Assembly Line
There is one master core which the other 17 core are attached to make a single mold for the cylinder block casting. Process of the cores assembly is done with the help of robots [8] and it’s a continuous process because a new mold is requiring for every new casting. 

3.6 Melting Aluminum Alloy
Aluminum alloy ingots are placed inside the gas fired furnace where temperature is about 800 degree centigrade. This process required careful handling due molted metal but this is continuous and a low cost process. 

3.7 Pouring
In manufacturing of engine cylinder block the process of pouring the molten metal for filling the mold cavity is done from the bottom to avoid the formation of oxide [8]. This process has usually had low labor and equipment and processing cost because of its automation. 

3.8 Sand Recovery Oven
After the solidification the mold is place in the sand recovery oven for six hours which dissolve all the glue present in the sand due to which all the sand is recovered. Sand present inside the cylinder block cavity can be removed my tilting the cylinder block side wise with the help of robotics [8]. This preprocess usually have low labor and processing cost associated with it because it can be done on many cylinder block molds in single time.

3.9 Primary Machining
After engine cylinder block is obtain form the sand recovery oven the process of machining is done to remove all the extra material present in the form of runner and riser and to provide some finishing to the engine cylinder block [8]. This process is usually done on the CNC machine have high equipment cost, and required skilled labor for processing but the high processing speed make it best for mass production processes [9].

3.10 Final Machining
Final machine is done by highly precise CNC machines due to high level of dimensional tolerance required for piston bores and all other parts. This process is usually done on the CNC machine have high equipment cost, and required skilled labor for processing but the high processing speed make it best for mass production processes [9].
 
4.0 Additive Layer Manufacturing Processes
Additive layer manufacturing technique manufacture a 3D product by adding layers of the materials one above the other that why this process is also known as layer by layer manufacturing. On the basis of the phase of the raw material used the additive layer manufacturing can be divided into three types 1. Liquid base processes 2. Powder base processes and 3. Solid base processes. Each of these processes is further divided into subtypes shown below

• Liquid Based Processes
1. Stereolithography Apparatus(SLA)

• Solid Based Processes
2. Fused Deposition Modeling (FDM)
3. Laminated Object Modeling(LOM)
4. Multi Jet Modeling

• Powder Based Processes
1. Selective laser Sintering(SLS)
2. Selective Laser Melting(SLM)
3. Zcorps 3D printer

All of the above mention additive layer processes have same number of steps involves in manufacturing of any product. Selection of a process for a product depends on the product requirements like material, ultimate tensile strength, density and performance of the product. Along with this some post process is required in some of the processes which should be considered while selecting the additive layer manufacturing process for a product. 

While selecting an additive layer manufacturing process for the engine cylinder block material is the most important factor because currently aluminum alloys are the standard material used for the process and some of available processes have limited range of process able materials. ‘

Second point the maximum ultimate tensile strength that can be achieved by the manufacturing the cylinder block through any of the process is also important because cylinder work under high temperature and stresses and ultimate tensile strength of some of the processes is limited. 

Density is also an important factor which contributes in proper functioning of product. Some of the process produces low density products and some produce full density products. Some of the additive layer process required post curing of the product, this factor should also be considered because of the cost involve in this process.  


Following is table that shows some of the features of the additive layer manufacturing processes [11].


Processes
Materials
Maximum UTS
Post Curing
Use
SLA
photopolymers
75 MPa
Required
Non-functional prototypes
SLS
Metals, ceramics and thermoplastics
1 GPa
Required
Functional components
SLM
Metals, ceramics and thermoplastics
> 1GPa
Not Required
Functional products
3D printing
Steel, bronze, ceramic,
5 MPa

Non-functional prototypes
FDM
Ceramic, Eutectic metals
>65 MPa
Not Required
Functional prototypes
LOM
Sheet of Metals, ceramics and thermoplastics
>60 MPa
Not Required
Non-functional prototypes
MJM
thermoplastics
<5 MPa

Non-functional prototypes

It clear that from the above comparison that selective laser sintering and selective laser melting can be used for the manufacturing of engine cylinder block as they can provide highest ultimate tensile strength and can process the required aluminum alloy. Selective laser melting has one advantage over selective laser melting that it does not required post curing of product and it can produce fully dense parts. 

So selective laser melting SLM is the process selected from all the available additive layer manufacturing process for the manufacturing of engine cylinder blocks due to its ability to manufacture fully dense engine cylinder blocks from aluminum alloys with maximum ultimate tensile strength.
 
5.0 Selective Laser Melting
Selective lase melting is an additive layer manufacturing process that make use of the laser power to completely melt the material present in the form of powder which on solidification makes a single very thin 3D layer of 2D cross section of a product. In this may layer after layer is added to make a complete 3D product. 

To manufacture an engine cylinder block through selective laser melting the steps are going to be the same that involve in the selective laser melting process. Following are the steps with details about the manufacturing of engine cylinder block through selective laser melting

5.1 Preparing CAD Model
First step in manufacturing of cylinder block through SLM is preparing a complete detailed CAD model of the cylinder block. This process required skilled labor but it is one time process with low equipment cost. This process may take days to a week. 

5.2 STL file Generation
Second step is converting the CAD model of cylinder block file into STL file which SLM machine can read. This is also a onetime process which is done by the same CAD preparing labor on the same CAD generating equipment and takes only few minutes.

5.3 Slicing the STL file
Third step is to slice the STL file into 2D cross section which is used by the machine to manufacture the layers while processing. These layers are combined to form a 3D product. This is also onetime process performed by same labor and equipment and takes only few minutes.

5.4 Preparations
Fourth step is to make all the necessary adjustment on the SLM equipment to start the manufacturing process. This process is needed to be done every time and have high labor cost and takes few minutes to hours.

5.5 Processing
Fifth step is the manufacturing process of cylinder block where machine manufacture layer after layer to complete a 3D physical product. This process required skilled labor and have very long processing time usually in day for a single product. For a product like cylinder block it may take weeks to complete. The equipment cost related to this process is very high.

5.6 Post Processing
After the manufacture process is completed the process of cleaning and finishing starts where extra powder and waste material is removed from the final product it a finished product. In SLM no post curing is required which make it little faster than the SLS. Post processing is continuous process which needs to be done every final product to make it a finished product. This process has moderate labor and equipment cost associated with it and have small processing time. 

6.0 Comparison between current and selected manufacturing process
As mention above the current manufacturing process of the cylinder block was sand casting that is being used by the company BMW and the recommended additive layer manufacturing process on the basis of the some factors discussed above is selective laser melting. Now both the process should be compared to check that the selected additive layer manufacturing process is economically better than the current manufacturing process. Following are some of the factors on which the comparison will be made

1. Number of Processing Steps
2. Time of Processing
3. Labor Requirements
4. Manufacturing Cost
5. Product Cost

6.1 Number of Process Steps
In sand casting of engine cylinder block there are about 10 man steps [8] where as in the selective laser melting process there are only six steps involves [11]. Therefore the manufacturing of cylinder block by the SLM will be much shorter than the current sand casting process.

6.2 Time of Processing
In sand casting of engine cylinder block the time of making the master molds is in months and then the time for sand core manufacturing and assembly to make a mold is in days for manual process and in hours for fully automatic process. Pouring, solidification and post processing may require days so complete manufacturing of cylinder block will be in days [12]. In SLM the there is no need of molds and cores so there lot of time saving in this process. In SLM melting and solidification occurs in seconds and also there is no need of post process [13] so SLM safe a lot of time as compared to sand casting

6.3 Labor Requirement
In sand casting there is requirement of highly skilled labor at every stage of cylinder block manufacturing [9] but in SLM a single labor can control the complete process [13] due to which SLM is quite economical and effective in this respective 

6.4 Manufacturing Cost
Due to less number of steps involve in SLM, the cost of manufacturing in SLM is less than the sand casting due to its high greater number of steps involves but the cost of the machine is a big problem in the way of this process installation. Cost of the SLM machine is about few million dollars

6.5 Product Cost
Cost of engine cylinder block produce by the SLM will be less than the one produce by the sand casting due to less number of steps involve, low processing time and less number of labor required for the production.

7.0 Conclusion
The objective of selecting an additive layer manufacturing process for the production of engine cylinder block has been successfully completed and selective laser melting is the process selected. Careful comparison of current and selected process shows that the production through the SLM process will have less processing steps with small processing time required for production. The required labor to carry out the process is also less as compared to sand casting. Due to all of the factor mention above the manufacturing cost and product will be lower than the one produce made by the sand casting. 
 
References
[1] Create it real (2012) 3D Printer Technology – Animation of layering [online] available at http://www.createitreal.com/index.php/technology/process 

[2] Excel. Jon (2010), the rise of additive layer manufacturing [Online] available at http://www.theengineer.co.uk/issues/24-may-2010/the-rise-of-additive-manufacturing/ 

[3] Farinia Group (n.d) what is Additive Layer Manufacturing (ALM) [online] available at http://www.farinia.com/additive-manufacturing/3d-technique/additive-layer-manufacturing 

[4] Hieu Nguyen (2005) Manufacturing Processes and Engineering Materials Used in Automotive Engine Blocks, School of Engineering Grand Valley State University, EGR250 – Materials Science and Engineering Section B

[5] What-When-How (n.d) Engine Construction [online] available at http://what-when-how.com/automobile/cylinder-block-automobile/ 

[6]Honda Manufacturing (n.d) High Pressure Die casting, Engine Manufacturing, [online] Available at http://www.hondamanufacturing.co.uk/our_plants/engine-manufacturing/high-pressure-die-casting/ 

[7] Cars (2015) BMW Engine Block Casting [online] Available at https://www.youtube.com/watch?v=N2hYTdrzujI 

[8] How its made (2013) How its Made Engine Blocks [online] Available at https://www.youtube.com/watch?v=wr4_B9EXWSo 

[9] K. G. Swift and J. D. Booker (2013) Machining Process, Manufacturing Process Selection Handbook, Elsevier Ltd, 

[10] Mikell P. Groover (2010) Chapter 11 Metal Casting properties, Fundamental of modern manufacturing materials, processes and system. 4th edition

[11] K. G. Swift and J. D. Booker (2013) Rapid Prototyping processes, Manufacturing Process Selection Handbook, Elsevier Ltd,

[12] K. G. Swift and J. D. Booker (2013) Metal Casting, Manufacturing Process Selection Handbook, Elsevier Ltd

[13] Ihar Yadroitsau (n.d) Direct Manufacturing of 3D Objects by Selective Laser Melting of Metal Powders